How to Read a Glass Liquor Bottle Spec Sheet (With a Worked Example)
A spec sheet is the contract between you, the glass plant and the bottler. Three numbers cause most of the trouble: brimful capacity, neck finish geometry, and weight tolerance. Read those first, then everything else.
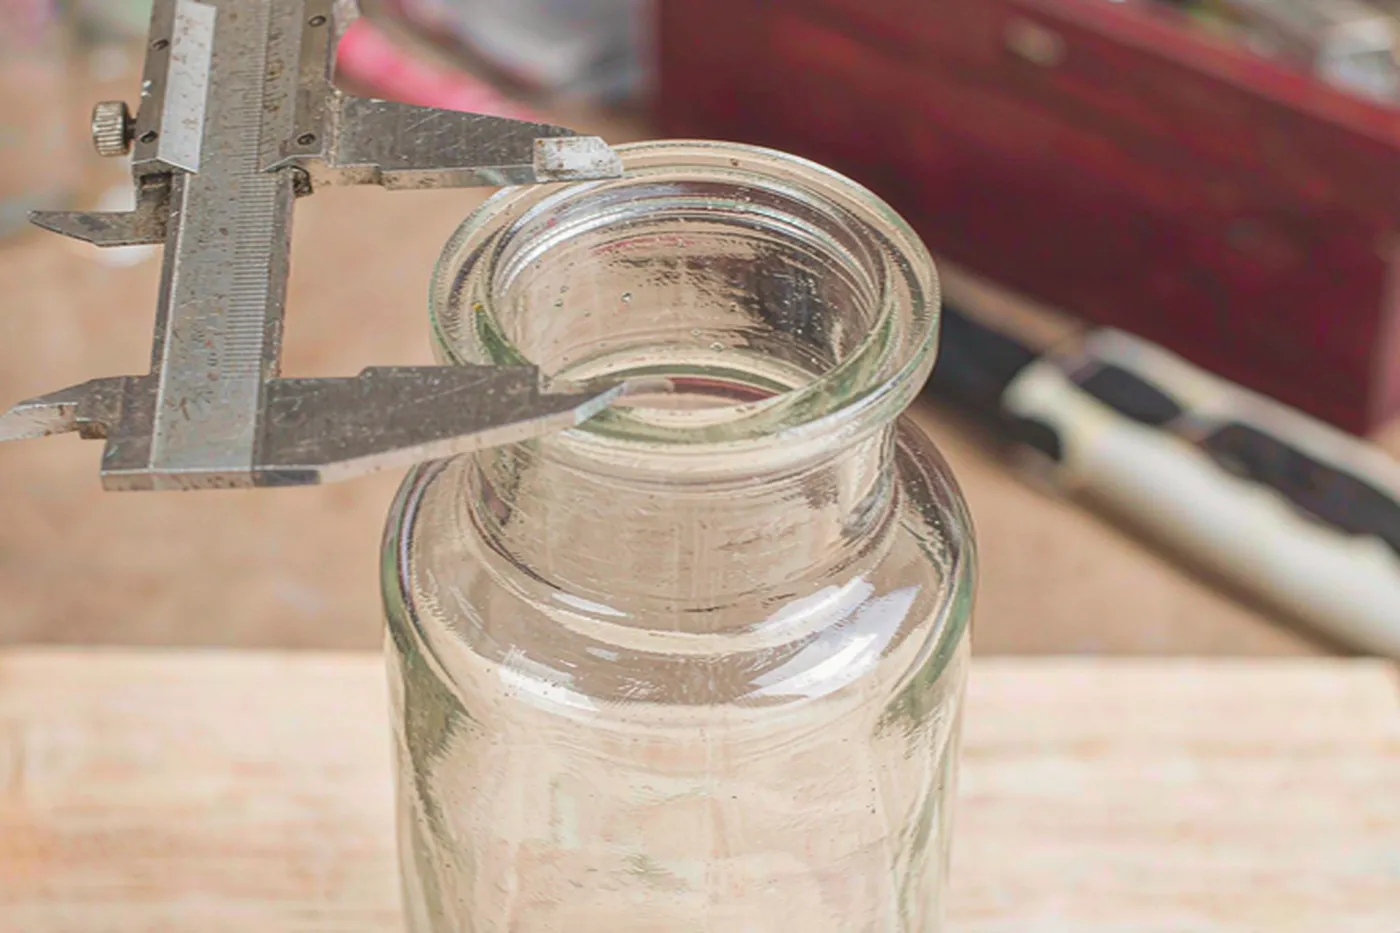

The fields that matter most
- Nominal fill — the volume you declare on the label, e.g. 700 ml.
- Brimful capacity — the physical volume to the rim, always above nominal fill.
- Weight — empty bottle mass in grams, with a tolerance.
- Overall height — drives carton and pallet design.
- Body diameter — drives labelling and carton fit.
- Neck finish — the closure interface, specified by a standard code.
Everything else on the sheet is secondary. If those six lines are right, the bottle can be quoted, tooled, filled and shipped.
Reading the neck finish
The finish is the most standardised part of the container, which is exactly why deviations are expensive. Two naming systems are in common use:
- GPI or CT codes — diameter then thread style. 28-400 means 28 mm outside thread diameter with a 400-style thread profile. A 28-400 cap will not thread onto a 28-410 neck even though the diameter is identical, so match both numbers.
- ROPP codes — metric diameters such as 25 mm, 28 mm, 30 mm and 31.5 mm, where a plain aluminium shell is rolled onto the glass thread at the filler.
- Bar-top and cork bores — straight-sided bores, with cork shank diameters commonly around 18.5 mm to 21.5 mm.
Critical drawing dimensions:
- T — outside thread diameter.
- E — thread root diameter.
- I — bore diameter. Critical for cork and bar-top shanks.
- S — top of finish to the start of the thread or bead. Controls seating and tamper-band clearance.
- H — finish or seat height.
Aluminium ROPP shells are far less forgiving than plastic continuous-thread caps. Where a tolerance is quoted for a threaded finish it is commonly around plus or minus 0.15 mm on the T dimension; outside that band the shell either spins free or splits its bridges during application. Confirm the actual figure on your drawing.
Fill, tolerance and headspace
- US spirits. Authorised metric standards of fill are listed in 27 CFR 5.203(a)(1): 1.8 L, 1.75 L, 1.00 L, 900 mL, 750 mL, 720 mL, 700 mL, 375 mL, 200 mL, 100 mL and 50 mL.
- Fill tolerance. Per TTB's gauging manual (SSD:TM:516, Rev. 6, issued 26 March 2025, implemented 9 April 2025): plus or minus 1.5 percent at 1 L and above; plus or minus 2.0 percent for 376 to 999 mL; plus or minus 3.0 percent for 101 to 375 mL; plus or minus 4.5 percent at 100 mL and below.
- Headspace. For containers of 200 mL or more, headspace cannot exceed 8 percent of total capacity (27 CFR 5.202(b)).
- EU spirits. Directive 2007/45/EC permits only nine nominal quantities between 100 ml and 2000 ml: 100, 200, 350, 500, 700, 1000, 1500, 1750 and 2000 ml.
Mechanical and thermal checks
Ask which standards the plant tests to and request the reports:
- Internal pressure — ASTM C147.
- Thermal shock — ASTM C149, commonly specified as surviving a sudden 42 degrees C drop.
- Vertical load — top-load strength needed to survive capping.
- Heavy metal release from decorated surfaces — ASTM C738 is commonly referenced.
A worked example
A brief for a 700 ml gin bottle might read:
- Nominal fill: 700 ml
- Brimful capacity: approximately 725 ml
- Weight: approximately 480 g
- Overall height: 300 mm plus or minus 1.5 mm
- Body diameter: 90 mm plus or minus 1.0 mm
- Finish: GPI 28-400 continuous thread
- Closure: aluminium ROPP 28 by 15.5 mm with tamper-evident band
- Colour: flint
From that single block the plant can quote tooling, the closure supplier can confirm compatibility, and the filler can set up the line. Most launch delays trace back to one of these lines being left blank and then guessed.
Tolerances that cause line stoppages
Most filling problems trace back to four dimensional issues:
- Overall height drift — causes misalignment under filling nozzles and capping heads. A typical planning tolerance is around plus or minus 1.5 mm, but the drawing governs.
- Lean or verticality — a leaning bottle tips under the capping head and can crack. Measured as deviation at the top of the finish.
- Bore variation — affects cork and bar-top compression fit, which then shows up as leakage or a sinking stopper.
- Finish T dimension — outside tolerance and an aluminium ROPP shell will not seal consistently.
Ask the plant which of these it measures in-process, at what frequency, and request the records for your batch.
Questions to ask the plant
- Which drawing revision is the quotation based on?
- What are the tolerances on overall height, body diameter and finish T?
- Which ASTM or ISO methods do you test to, and can I see the latest reports?
- Is the bottle validated for the filling method and line speed I use?
- Can you provide batch traceability linking test reports to the shipped goods?
A short specification template
- Capacity: nominal fill and brimful capacity, each with tolerance
- Weight: target and tolerance
- Dimensions: overall height, body diameter, each with tolerance
- Finish: standard code plus T, E, I, S, H
- Colour: reference code and batch tolerance
- Tests: internal pressure, thermal shock, vertical load, heavy metal release if decorated
- Packing: carton specification, units per carton, pallet pattern
Errors that appear on real spec sheets
- Capacity given without stating whether it is nominal or brimful — the most common and the most consequential.
- Finish described by diameter only, omitting T, E, I, S and H.
- Tolerances listed for some dimensions and not others, which usually means the missing ones are uncontrolled rather than tight.
- No drawing revision or date, so no one knows which version the quotation covered.
- Decoration described without saying which surfaces, which matters for testing scope.
Each of these is a documentation failure rather than a manufacturing one, and each is fixable at the drawing stage.
A worked specification, end to end
Pulling the fields together for a 700 ml premium spirits bottle:
- Capacity: 700 ml nominal, brimful capacity to the drawing with tolerance
- Weight: target with tolerance
- Height and body diameter: each with tolerance
- Finish: code stated in one system, plus T, E, I, S and H
- Colour: reference code, batch tolerance, and the cullet ratio the plant will run
- Tests: vertical load, internal pressure, thermal shock, heavy metal release on decorated areas
- Packing: carton specification, units per carton, pallet pattern
Every line is checkable at goods-in. That is the test of whether a specification is complete.
Key takeaways
- Brimful capacity, neck finish geometry and weight tolerance cause most filling problems - read those first.
- T, E, I, S and H are the five finish dimensions that decide whether a closure fits.
- Height drift, lean, bore variation and finish T are the four tolerances that stop lines.
- A drawing with no revision number, no date or incomplete tolerances is not a specification.
- Ask which tolerances the plant measures in-process, how often, and for the records.
- A complete specification is one where every line is checkable at goods-in.
Frequently Asked Questions
What does brimful capacity mean?
Brimful capacity is the volume the bottle holds when filled to the very top, before any closure is applied. It is always larger than the nominal fill, and the difference is the headspace.
What is the difference between nominal fill and overflow capacity?
Nominal fill is the volume declared on the label and used for trade. Overflow, or brimful, capacity is what the container physically holds to the rim, and it is always the larger number. The gap between them provides the headspace needed for thermal expansion and for the fill-height tolerance the filling line can hold.
What are the T, E, I, S and H dimensions on a neck finish drawing?
T is the outside thread diameter, E is the thread root diameter, I is the bore, S is the distance from the top of the finish to the start of the thread or bead, and H is the finish height or closure seat height.
How much height variation is normal?
Dimensional tolerances are set per drawing rather than by category, so there is no universal figure. A typical planning figure for overall height on a spirits bottle is in the region of plus or minus 1.5mm, but the drawing governs.
Why is vertical load strength specified?
Automated capping heads press down on the finish, and stacking in the warehouse adds further top load. If the bottle cannot carry that load it will crack or shatter on the line, or fail in the pallet stack. The figure belongs on the drawing as a stated minimum, not left to the plant to interpret.
What is verticality or lean tolerance?
It is the maximum permitted deviation of the bottle axis from true vertical, usually expressed in millimetres over the full height. Excessive lean causes filling and capping misalignment on high-speed lines, and it makes the bottle look visibly crooked when several stand together on a shelf. Specify it with a tolerance and check it at goods-in.
Do I need the finish drawing before choosing a cap?
Yes. The finish drawing fixes the diameter, thread profile and T, E, I, S and H dimensions that any closure must match, and a closure chosen from a nominal size alone will often fail at sealing. Send the drawing rather than just a code to the closure supplier before you commit.
Related
- Standard vs Custom Mould: Cost, Lead Time and Break-even for Spirits Bottles
- Liquor Bottle Sizes and Capacity Guide: 50ml to 2000ml Compared
- Liquor Glass Bottle Buyer's Guide 2026: Capacity, Glass Type, MOQ and Cost
Written by Liang Wei, Glass Packaging Engineer.